
Crystallization is one of the most critical stages in sugar production. It directly affects product quality, process yield, energy consumption, water usage, and final molasses purity. Poor crystal size distribution, excessive fines, and uncontrolled crystal growth can reduce product quality and increase operating costs.
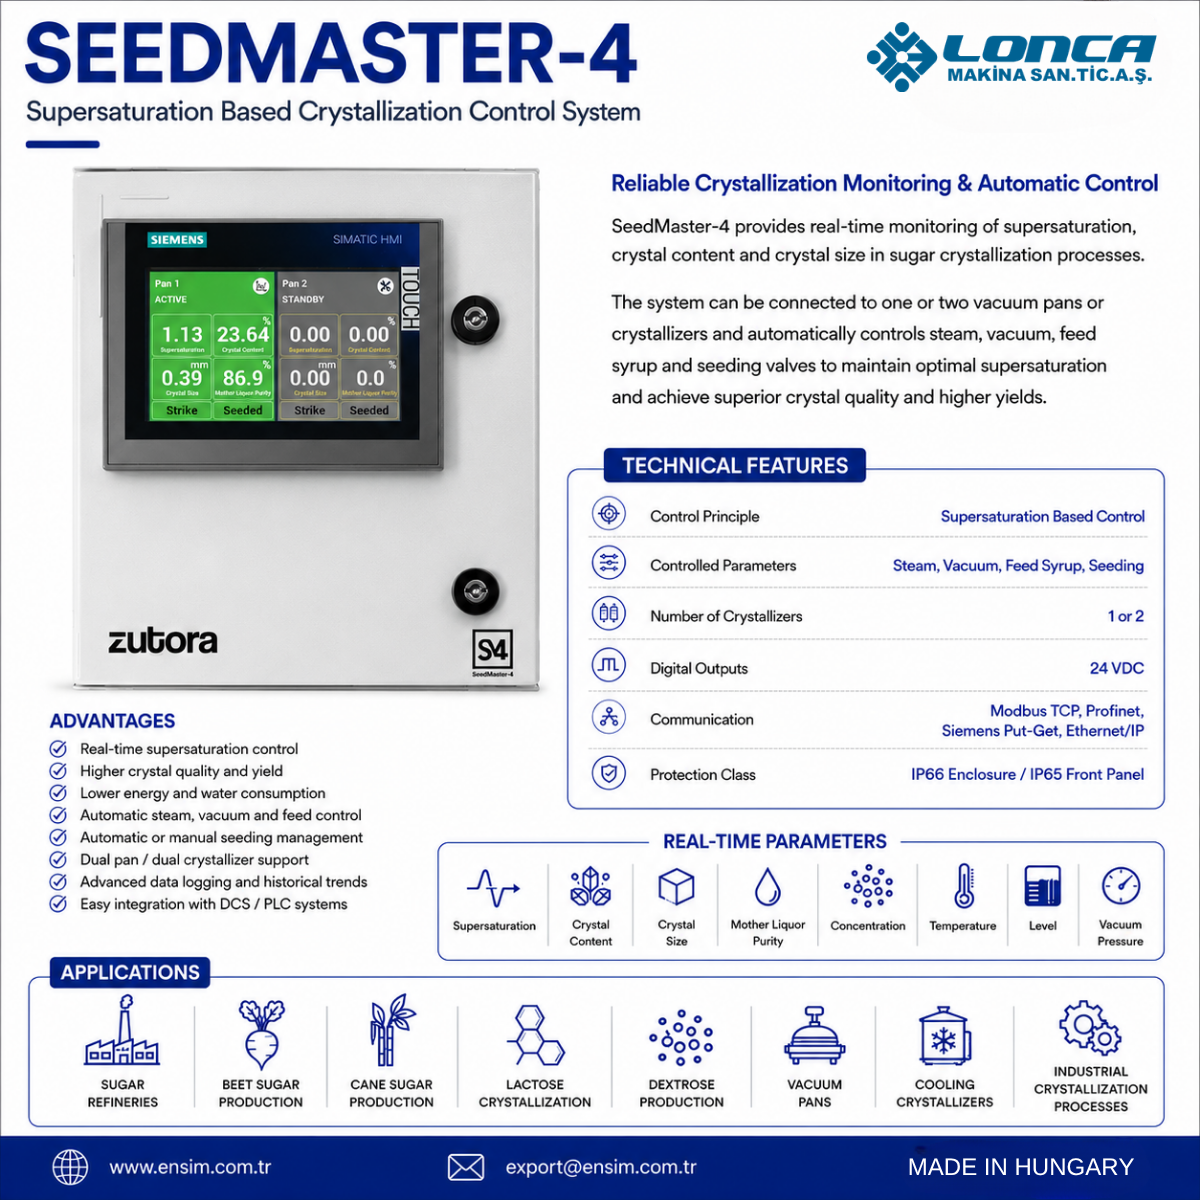
SeedMaster-4 is designed to solve these challenges by providing real-time, in-line monitoring and advanced control of crystallization based on supersaturation. By keeping supersaturation within the optimal range throughout the batch, SeedMaster-4 helps sugar factories achieve more consistent crystal quality, improved yield, and more efficient operation.
Why Crystal Quality Matters
Poor crystal quality creates several problems in sugar production. A weak crystal size distribution can lead to product quality issues, higher recirculation rates, and unnecessary consumption of energy, time, and water.
Fines and conglomerates can be especially problematic. If a batch contains too many fine crystals, they may pass through the centrifuge screens with the runoff syrup and enter the final molasses. This increases molasses purity and therefore increases sugar losses.
Maintaining a narrow and consistent crystal size distribution is one of the key targets of efficient crystallization. SeedMaster-4 supports this goal by using supersaturation as the main control parameter.
The Role of Supersaturation in Crystallization
Supersaturation is the driving force behind both nucleation and crystal growth. If supersaturation is too low, the solution becomes undersaturated and crystals may dissolve. If supersaturation is within the metastable zone, crystal growth can occur in a controlled and stable way.
However, if supersaturation becomes too high, the process may enter intermediate or labile zones where spontaneous and secondary nucleation can occur. This results in fines, poor crystal size distribution, and reduced crystal quality.
For this reason, high-quality crystallization requires supersaturation to be kept within the metastable zone throughout the batch. SeedMaster-4 is developed specifically to monitor and control this condition.
What Is SeedMaster-4?
SeedMaster-4 is a crystallization transmitter and control device for sugar production. It provides accurate, real-time, in-line monitoring of critical massecuite and crystallization parameters, including supersaturation and crystal content.
The system can be connected to one or two crystallizers. It is suitable for batch vacuum pans and batch cooling crystallizers, depending on the selected model. Advanced versions include a supersaturation-based control system that can control key process variables automatically.
Applications
SeedMaster-4 can be used with cane sugar, beet sugar, lactose, and dextrose applications. It is suitable for both high-purity and low-purity crystallization processes.
Typical applications include refinery pans, raw sugar crystallization for A, B, or C strikes, molasses exhaustion, and C massecuite cuts. In high-purity applications, the main benefits include improved crystal quality and yield, along with reduced energy and water usage. In low-purity applications, such as C massecuite crystallization, one of the most important benefits is the reduction of final molasses purity.
Real-Time Key Parameters
SeedMaster-4 provides reliable online data for key crystallization parameters. These include supersaturation, crystal size, crystal content, and mother liquor purity.
Additional data is collected from accurate instruments mounted on the pan, including mother liquor concentration, temperature, total solids, and level. The system ideally works with a process refractometer, a microwave probe, and a level sensor to provide a complete real-time picture of the crystallization process.
This data allows operators and control systems to understand the process more accurately and make better decisions during each batch.
Supersaturation-Based Control
Basic SeedMaster models monitor supersaturation and other important crystallization parameters. Control versions apply an advanced supersaturation-based crystallization control strategy.
When used with vacuum pans, SeedMaster can control steam, vacuum, feed syrup, and seeding to keep supersaturation within the optimal operating range. For cooling crystallizers, the system can control temperature and seeding.
This approach helps prevent excessive supersaturation, minimizes secondary nucleation, supports controlled crystal growth, and improves product consistency from batch to batch.
Control of Steam, Vacuum, Feed Syrup, and Seeding
SeedMaster-4 advanced control versions use the supersaturation signal to influence multiple process variables. Steam control affects evaporation and mother liquor concentration. Vacuum control affects absolute pressure and massecuite temperature. Feed syrup control manages pan level and growth conditions. Seeding control ensures that seed crystals are introduced at the correct supersaturation level.
By coordinating these control actions, the system helps maintain the crystallization process in the desired operating zone and reduces dependence on manual operator judgment.
SeedMaster-4 Models
The SeedMaster-4 family includes different models for sugar beet and cane sugar applications.
SM4-SV is designed for batch vacuum crystallizers and provides a supersaturation setpoint signal. SM4-SV-ACC includes advanced control for batch vacuum crystallizers. SM4-SC is designed for batch cooling crystallizers, while SM4-SC-ACC includes advanced crystallization control for batch cooling crystallizers.
This model structure allows factories to select a monitoring-focused or advanced control-focused solution according to their process requirements.
Hardware and User Interface
The SeedMaster SM4-S-V-ACC system is built in a wall-mounted cabinet and includes a Siemens S7-1200 series PLC, analog input and output modules, an industrial Ethernet switch, a secure VPN router, and a Siemens SIMATIC touchscreen HMI.
The HMI displays the most important values for one or two pans. The main screen shows pan status, supersaturation, supersaturation setpoint, concentration, concentration setpoint, steam valve output, absolute pressure, vacuum valve output, level, feed valve output, crystal content, crystal size, mother liquor purity, strike status, and seeded status.
The system uses clear operating states such as standby, active, and error, allowing operators to monitor the crystallization process in real time.
Required Instruments
For accurate supersaturation calculation and control, SeedMaster-4 requires reliable measurement inputs. A VAISALA K-Patents process refractometer is mandatory for mother liquor concentration and massecuite temperature.
The system also requires a third measurement input, which can be massecuite solids content from a microwave probe or density from a density probe. A well-calibrated microwave probe is preferred. Level measurement is also mandatory, and absolute pressure measurement is required when vacuum or pressure control is used.
Communication and Integration
SeedMaster-4 can integrate with factory control systems through analog outputs, digital outputs, and Ethernet-based fieldbus systems. Supported fieldbus options include Modbus/TCP, Profinet, Siemens Put-Get, and Ethernet/IP.
The system can transmit important crystallization parameters such as supersaturation, crystal size, crystal content, mother liquor purity, concentration, temperature, total solids, density, and valve control signals. This makes it suitable for both standalone operation and integration into existing plant automation systems.
Data Logging and Process Analysis
SeedMaster-4 logs process data once per minute for each strike. Logged values include concentration, temperature, level, massecuite solids content, density, absolute pressure, supersaturation, crystal content, crystal size, mother liquor purity, setpoints, and valve outputs.
Logs are stored in CSV format and can be opened in Microsoft Excel for further analysis. This allows factories to review strike history, compare batch performance, and support continuous process improvement.
Remote Support Capability
The SeedMaster-4 system includes a secure VPN router for remote support. By default, remote access is disabled and must be enabled by the operator. When authorized, Zutora engineers can connect securely for service and software support.
This feature helps reduce downtime and allows technical assistance without requiring immediate on-site intervention.
Benefits for Sugar Factories
SeedMaster-4 helps sugar factories improve crystallization performance by keeping supersaturation under control. This supports more uniform crystal growth, improved crystal size distribution, and reduced formation of fines.
The system also helps reduce water consumption because fewer fines need to be dissolved during crystallization. More uniform crystals can reduce washing water demand in batch centrifuges. In low-purity applications, supersaturation-based control can significantly reduce final molasses purity and therefore improve sugar recovery.
Conclusion
SeedMaster-4 is an advanced supersaturation-based crystallization monitoring and control solution for the sugar industry. By combining real-time measurement, intelligent control, process visualization, data logging, and automation integration, it helps factories improve crystal quality, reduce losses, and optimize crystallization performance.
For sugar producers seeking better batch consistency, improved yield, lower water and energy usage, and stronger process control, SeedMaster-4 provides a powerful and practical solution for modern crystallization management.